If you’ve ever had a part so precise it could only be made with a lathe, you’ve probably wondered how the automatic version works—especially since it’s the workhorse for everyone from small machine shops to big automotive part lines. As someone who’s spent the last 12 years supplying these machines (and troubleshooting the weird, last-minute jams that throw a whole production day off), I can tell you it’s not just one magic part—there are 5 core components that make an automatic lathe actually automatic. Let’s break them down like I would when walking a new customer through our showroom floor, no stuffy jargon, just real talk. Automatic Lathe
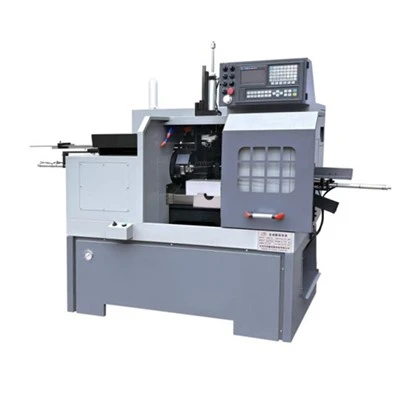
First, let’s get one thing straight: when people say “automatic lathe,” they don’t mean it runs without any human check-ins—they mean it switches between parts, changes tools, and feeds raw material all on its own, so a single operator can tend 2 or 3 of them at once. If you’re used to manual lathes, this is a game-changer, but the secret isn’t flashy tech—it’s the foundational parts that work together like a well-oiled team. Let’s start with the one that makes the whole thing turn: the main spindle unit.
The main spindle is literally the heart of the machine. It’s what holds your raw material—bar stock, usually, since automatic lathes are built for high-volume runs—and spins it at the exact speed you need, like 500 RPM for soft aluminum or 2,000+ RPM for hard steel. Here’s the thing most new buyers don’t realize: a bad spindle makes even the best automatic lathe garbage. If it wobbles (you’ll see this in test cuts as uneven circles), every part you make will be out of spec. I’ve had customers come to me after buying a cheap lathe online, complaining that their parts are failing inspection, and 9 times out of 10, it’s a low-quality spindle. Our spindles are precision-ground, with ceramic bearings that last 10,000+ hours, and we test every single one before it leaves our warehouse—no surprises. The spindle also connects to the feed mechanism, which is the part that pulls new bar stock into the machine when a run is done. That feed mechanism isn’t a fancy robot arm—it’s a set of clamps and a lead screw that moves the bar stock forward by the exact length needed for each part. If the feed is off by even 0.1mm, you scrap a whole batch. This is why we calibrate the feed system on every machine before delivery; it’s not optional for us, because we’ve seen too many shops lose money to bad calibration.
Next up, the tool turret—this is the part that actually cuts, drills, or shapes the raw material. Think of it like a rotating lazy Susan, but instead of holding condiments, it holds 8 to 16 different cutting tools (drills, end mills, face mills, even threading taps) that the machine switches between in seconds. Here’s where the “automatic” part clicks: the turret knows when to stop spinning, lock in place, and bring the right tool to the spindle for each step of the part. For example, if you’re making a tiny bolt, the turret will first use a roughing tool to cut the outside of the bolt, then switch to a finishing tool to get the threads exact, then a drill to make the hole for the bolt’s center. The best turrets are indexable—meaning they rotate fast without bouncing, so you don’t get tool marks on the part. We use servo-driven turrets, not the old hydraulic ones that slow down over time; our customers love that they can switch tooling between part runs in 2 minutes, no need to adjust belts or anything. A common mistake shops make with turrets is using cheap, dull tools—even the best turret can’t save you if the cutting edges are worn. We always recommend pairing our lathes with high-quality carbide tools, and we have a parts kit for that, so customers don’t have to hunt around for something that works.
Then there’s the control system—this is the brain of the whole operation, and it’s the part that separates a basic automatic lathe from one that can handle complex, custom runs. Back in the day, automatic lathes used punch cards or old analog dials, and if you wanted to make even a tiny change to a part, you had to re-program a whole new card, which cost hours. Now, it’s all CNC (Computer Numerical Control) — that’s the control system we use. The operator just types in the part specs, like “0.5-inch diameter, 1-inch long, 16 threads per inch,” and the CNC does all the calculations for the spindle speed, turret positions, and feed rates. Here’s the perk for small shops, not just big factories: our CNC systems are user-friendly, even if your operator isn’t a computer genius. We pre-load common part programs, so if you make bolts all the time, you just pull up the bolt program, adjust the length, and go. No more spending a whole day programming a new run. The control system also has safety features—like if a tool breaks, it will stop the machine before it damages the spindle or turret, which saves shops from thousands of dollars in repairs. I once had a customer who forgot to change a dull drill, and the CNC stopped the machine before it bent the drill, so he only had to replace a $5 drill bit instead of a $2,000 tool holder. That’s the stuff that matters.
Fourth, we have the coolant and lubrication system—this is the unsung hero of automatic lathes, because everyone remembers the big parts, but if this breaks, the whole machine seizes up in minutes. When you’re cutting metal at high speeds, the cutting tool and the part get super hot—like, hot enough to warp the part or dull the tool in 5 minutes. The coolant system sprays a mix of water and cutting oil directly on the cutting area to keep things cool, and also flushes away metal shavings (called swarf) so they don’t get stuck between the tool and the part. The lubrication system is different—it oils all the moving parts: the spindle bearings, the turret gears, the feed screw. If you don’t lubricate those, they wear out way faster. We use a closed-loop coolant system for our lathes, which means the coolant is filtered and reused, so shops save money on fluid and don’t have to dispose of it as much. A lot of cheap automatic lathes have open systems where coolant gets contaminated with swarf right away, so you’re changing it every week. Our customers go 3 months between coolant changes, which is a huge win for their bottom line. We also have a filter indicator on the control system, so you know when it’s time to replace the filter, no guesswork.
Last but definitely not least, the part ejection and chip handling system. Once the part is done—say, a bolt or a small engine component— it needs to be moved out of the machine so the next part can be made. That’s where part ejection comes in: a small arm or clamp pushes the finished part out of the spindle, usually into a bin or a conveyor that takes it to a inspection station or packaging area. Then there’s the chip handling, which is for all the metal shavings from cutting—those can be sharp, oily, and if they pile up, they can jam the machine or even cause a fire if they get too hot. Our lathes have a chip conveyor that pulls all the shavings out of the machine and into a separate bin, so you don’t have a bunch of swarf clogging up the work area. This is especially important for high-volume runs, like making 10,000 parts a day—you don’t want an operator stopping every hour to pick up shavings. We even have optional part counting, so you can check how many parts you’ve made without walking over to the machine, which is a big help for shops running multiple lathes at once.
Now, let’s talk about how all these parts work together, because that’s what makes an automatic lathe actually automatic. You load a bar stock into the spindle, set the program on the CNC control, turn on the coolant and lubrication, and hit start. The spindle spins the bar, the turret moves the roughing tool into place, cuts the first pass, then switches to the finishing tool, drills a hole, cuts threads—all while the feed system pulls new bar stock forward. When the part is done, the ejection arm pushes it out, the chip conveyor carries away the shavings, and the whole thing starts over for the next part. No one has to stand there changing tools or feeding stock, which is why these machines are so valuable for shops that need to make a lot of parts fast, without hiring extra operators.
I know a lot of small shop owners are nervous about automatic lathes—they think they’re too complicated, or they’ll be stuck with a machine that can’t adjust if they get a custom order. That’s why we designed our lathes with modular parts, so if you need to switch from making bolts to making small brackets, you can change the turret tools and adjust the CNC program in an hour, not a full day. We also offer on-site training for every customer, and we have 24/7 tech support—if your operator has a question at 2 a.m. during a big run, they can call someone and get help, no waiting. We don’t sell machines and disappear; we’re in this with our customers for the long haul.
If you’re tired of manual lathes that require 2 operators to keep up, or you’ve been dealing with cheap automatic lathes that break down every few months, let’s chat. We can send a demo machine to your shop so you can test it with your actual parts, no pressure, no hard sell. Just reach out to our team, and we’ll work with you to find the right automatic lathe for your production needs—whether you’re making 100 parts a month or 10,000 a day.
5 Axis Machining Center References
- "Automatic Lathe Components and Operation" – Manufacturing Engineering Magazine, 2022
- "CNC Machining Fundamentals" – Society of Manufacturing Engineers, 2021
- "Coolant and Lubrication Best Practices for Metal Cutting" – Machinist’s Workshop Journal, 2023
- "High-Volume Turning Technology" – Modern Machine Shop, 2022
Taizhou Qiyang Trading Co., Ltd.
As one of the most professional automatic lathe manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk automatic lathe for sale here and get quotation from our factory. Customized orders are welcome.
Address: Zhenhai Village, Binhai Town, Wenling City, Taizhou City, Zhejiang Province
E-mail: qycncmachine@outlook.com
WebSite: https://www.qycncmachine.com/
