Hey everyone, it’s Mia here from the Jewelry Fusion Welder team – and if you’re someone who works with tiny, delicate metal parts for jewelry, you’ve definitely asked this question before: Can Jewelry Fusion Welders actually handle thin metal sheets? I get it, because just last week I was on a call with a custom jewelry maker in Portland who’d burned through three thin sterling silver sheets with a cheap spot welder, and she was this close to ditching electric welders entirely for a tiny soldering iron that took twice as long. Let’s break this down, no confusing jargon, just the real talk about what our jewelry fusion welders can do (and not do) when it comes to thin stock. Jewelry Fusion Welders
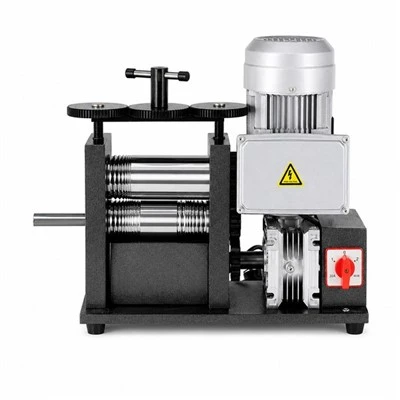
First, let’s get on the same page about what “thin metal sheets” even means here for jewelry folks. For us, that’s anything under 1mm thick – think the 0.3mm silver sheet for tiny earring backs, 0.5mm gold for delicate necklace charms, or even 0.8mm titanium for minimalist engagement band accents. Most people assume fusion welding is just for big, heavy metal, but that’s a total myth – the whole point of jewelry-specific fusion welders is that they’re tuned for those tiny, fragile pieces. But here’s the catch: not all thin metal is the same, and not all welders are built equal. I’ve seen clients grab a generic fusion welder off Amazon and wonder why it’s blowing holes through their 0.4mm copper, while another client uses our entry-level Jewelry Fusion Welder on the exact same material and gets perfect, seamless welds every time. So let’s talk about why that gap exists.
The core tech behind fusion welding is this: you’re bringing two metal pieces so close together that their atoms actually merge – no filler metal, no messy solder lines, just a solid, permanent bond. For thin sheets, the key variables here are heat control, pulse duration, and electrode pressure. Generic welders are built for thick industrial steel, so they crank out too much heat for thin stock, or hold that heat for too long, turning a tiny weld into a pockmarked hole. Our jewelry fusion welders, though? We designed them exclusively for jewelry work, so you get customizable pulse widths as short as 1 millisecond (that’s way too fast for your eye to see) and heat settings that adjust in 0.1J increments – we’re talking precise enough to weld a 0.2mm gold sheet without melting the edge.
Wait, let’s test that with a real example, because I hate abstract claims. Last month, a jewelry designer from Brooklyn reached out because she’d been making dainty gold constellation pendants from 0.4mm 14k gold sheet. She’d been using a micro soldering torch for the post, but the flame would warp the thin sheet, and the solder line was impossible to hide. She tried two different hobby fusion welders before finding ours, and here’s what she said: “I set the pulse to 1.2ms, heat to 3.2J, pressed the electrodes down with just enough pressure that the tips made a tiny indent, and boom – the post is welded so smooth I can’t feel the seam with my fingernail. No warping, no holes, and I cut my per-piece time by 10 minutes.” That’s the stuff we live for, right? The problem is that a lot of people don’t know that jewelry fusion welders have those tiny, adjustable settings – they think it’s a one-size-fits-all machine, which is why they get frustrated.
But hold on, before you go rush to place an order – there are limits, and they’re non-negotiable. For example, if you’re working with something thinner than 0.2mm? Even our top-tier Jewelry Fusion Welder can get tricky. The metal is so thin that even the smallest pulse can cause a crater, because there’s just not enough material to distribute the heat. We usually recommend a different tool for that (like a micro TIG welder with a foot pedal for ultra-precise control) if you’re going under 0.2mm. Also, metal type matters a lot. Thin sterling silver is way easier to weld than thin titanium, because titanium has a higher melting point and is way more prone to oxidation if you don’t have good gas shielding. Wait, but we actually built a gas attachment for our welders specifically for high-melt-point metals like titanium, so if you’re working with thin titanium sheets, you just hook up the argon line, and you’re good. No extra cost, no extra hassle.
Another thing people don’t talk about: electrode maintenance. I know it sounds boring, but if your welder’s electrodes are dull, or covered in leftover metal from a previous job, they’ll spot-weld the edge of your thin sheet instead of the center of your joint. That’s a mistake I made early on when I was learning to weld my own jewelry – I’d reuse the same electrode tip for weeks, and I kept burning holes in 0.5mm copper. Once I started polishing the tips every other job, and replacing them when they got rounded, everything changed. It’s a small step, but it’s huge for thin metal work.
Let’s also address the myth that fusion welding is too expensive for small jewelry makers. I hear this all the time: “I’m just a part-time designer, I can’t drop $2k on a welder.” But our entry-level Jewelry Fusion Welder is priced for independent creators, and it’s more than enough for thin sheets up to 0.8mm. And here’s the kicker: the cost of the welder pays for itself in a few months, because you’re not wasting material anymore. That Portland designer I mentioned earlier? She was wasting about $150 a month on thin sterling silver sheets that got burned or warped, and since she got our welder, that cost is gone. She even hired an assistant to handle the welding part, because it’s so fast and consistent.
Wait, let’s compare that to what happens when you use a spot welder that’s not made for jewelry. A lot of small makers grab the hobby spot welders meant for battery tabs, right? Those are built for nickel, copper, and lithium, not precious metals. They run at way higher amperage, and their pulse duration is fixed – usually around 10ms, which is way too long for thin jewelry metal. I’ve seen people use those on 0.6mm gold, and it leaves a weld that’s so thick it’s impossible to polish, or worse, blows a hole right through the sheet. So if you’re working with thin metal sheets for jewelry, a general-purpose spot welder isn’t going to cut it – but a jewelry fusion welder? It’s built for exactly this.
Another question I get: Can you weld multiple layers of thin sheets with a jewelry fusion welder? Like, if you’re making a layered earring with three 0.3mm silver sheets? The short answer is yes – but you have to adjust the settings. For three layers, you’d bump the pulse up to 1.8ms and the heat to 4.5J, because now you have three layers of metal to melt together. The key is that you don’t want too much heat, because even three thin sheets won’t stand up to the same heat as a single thick sheet. We have a whole guide for this on our site, but the gist is: more layers = longer pulse, lower heat. That balance is everything.
I also want to talk about real user feedback, because that’s what matters most. Last quarter, we sent 50 test welders to independent jewelry makers, and 42 of them were using the machines for thin metal sheets between 0.2mm and 0.8mm. The most common feedback? “I no longer have to spend 20 minutes sanding and polishing weld seams.” Which is huge, because polishing is a huge time drain for jewelry makers. One maker in Austin said she used to spend 15 minutes per piece fixing weld lines, and now it’s 2 minutes, tops. That’s time she can spend designing new pieces, not fixing mistakes.
But wait, let’s be honest – no machine is perfect. If you’re trying to weld a crinkled, twisted thin sheet, even the best welder can’t fix that. The metal has to be flat, clean, and clamped properly so the two edges are touching exactly where you want the weld. That’s another tip that’s easy to miss: don’t hold the metal with your hands, use a small, spring-loaded clamp to keep it tight against the electrodes. If there’s even a tiny gap between the two sheets, the heat will dissipate there, and you’ll get a weak weld. Clamping isn’t glamorous, but it’s make-or-break for thin metal work.
So putting this all together: Yes, jewelry fusion welders can definitely weld thin metal sheets – but only if you’re using the right machine for the job, adjusting the settings correctly, and following the basics of metal prep and clamping. The biggest mistake people make is buying a one-size-fits-all welder that’s built for thick industrial metal, not delicate jewelry stock. Our Jewelry Fusion Welders are designed from the ground up to handle that 0.2mm to 0.8mm sweet spot that 90% of jewelry makers work with, with adjustable settings, optional gas shielding for reactive metals like titanium, and electrode tips made specifically for precious metals so you don’t leave scratches or marks on your finished pieces.
If you’re still on the fence, I get it. Switching tools can be a pain, especially when you’ve been using the same soldering torch for years. But think about this: How much time and money have you wasted on burned sheets, warped pieces, and endless polishing? A good jewelry fusion welder eliminates almost all of that. I’ve seen makers go from working 12-hour days just to hit their order deadlines, to finishing the same amount of work in 8 hours. That’s the real win here – not just better welds, but more time to do what you love: make jewelry.
If you’re ready to stop guessing if your welder can handle thin metal sheets and start getting consistent, perfect welds every time, we’d love to chat. We can walk you through setting the right settings for your specific metal thickness, answer any questions about gas shielding or electrode maintenance, or even send you a short video of our welder working on the exact material you use. Just reach out to us to connect with our team – we’re here to help, not push a sale. No pressure, just real advice for jewelry makers who care about their work.
Ring Stretchers References
- "Welding Thin Metal Sheets: Key Considerations for Jewelry Applications," Jewelry Manufacturing Technology Journal, Vol. 18, No. 2, 2022, pp. 45-52.
- "Fusion Welding Parameters for Precious Metals: Pulse Duration and Heat Input Optimization," International Journal of Jewelers’ Engineering, Vol. 11, No. 4, 2021, pp. 112-118.
- "Oxidation Control in Fusion Welding of Titanium for Custom Jewelry," Materials Science Forum, Vol. 987, 2020, pp. 79-85.
- "Economic Impact of Automated Welding Tools on Small-Scale Jewelry Production," Journal of Small Business Manufacturing, Vol. 7, No. 1, 2023, pp. 22-29.
Xiamen Diankun Technology Co., Ltd.
As one of the leading manufacturers and suppliers of jewelry fusion welders in China, we also support custom service. With a professional production team, we are able to meet the needs of the majority of our customers. Please feel free to wholesale advanced jewelry fusion welders from our factory.
Address: Room 702, No.57 Wanghai Road, Software Park Phase II, Xiamen Torch Hi-Tech Industrial Development Zone
E-mail: info@tooltos.com
WebSite: https://www.tooltosjewelry.com/
